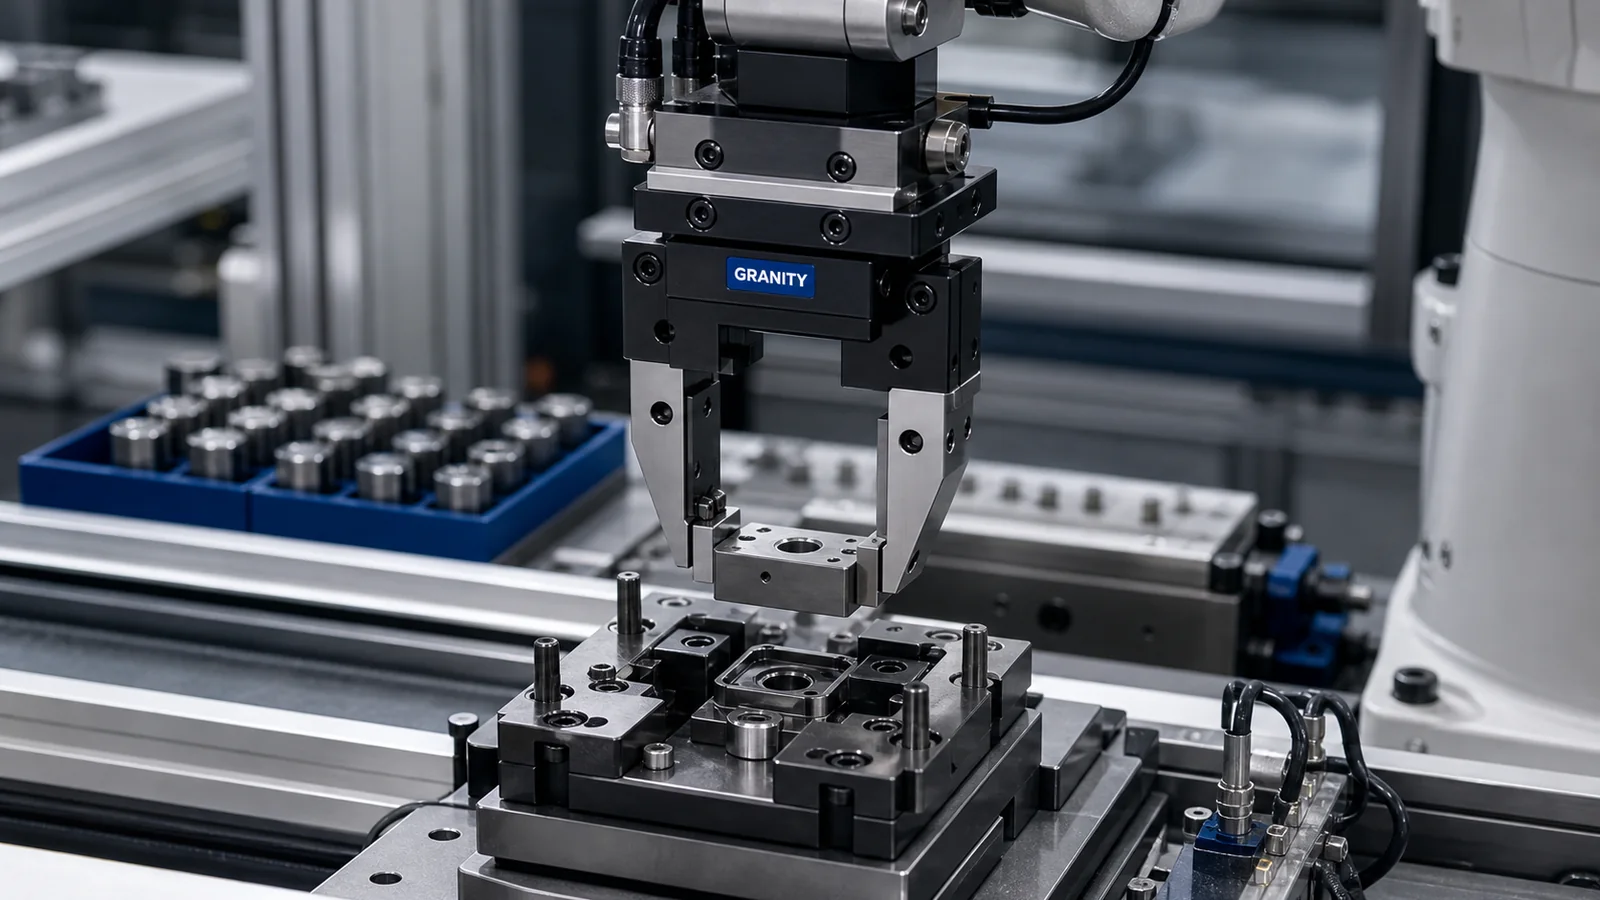
Machine TendingCNC loading and unloading
Define raw and finished part states, gripper approach, machine access, door behavior, workholding method and output sequence before product selection.
- Relevant products: grippers, tool changers, zero point systems
- Recommended next step: engineering review before RFQ
AssemblyPart handling and placement
Assembly applications often require careful review of part orientation, surface protection, insertion direction, sensor confirmation and cycle expectations.
- Relevant products: parallel grippers, angular grippers, compensation units
- Recommended next step: CAD request or engineering review
Fixture SetupRepeatable workholding changeover
Fixture changeover projects should define machine table, fixture size, stack height, datum logic, actuation preference and contamination conditions.
- Relevant products: zero point systems, workholding clamps
- Recommended next step: quote request with machine and fixture context
InspectionPositioning before measurement
Inspection workflows may need gentle gripping, repeatable location and clear access to measured surfaces without blocking measurement features.
- Relevant products: grippers, fixtures, compensation units
- Recommended next step: engineering review
Flexible CellsMulti-tool automation
Flexible automation cells should review tool variety, storage concept, utility pass-throughs, robot payload and future expansion before finalizing the tool side.
- Relevant products: tool changers, pneumatic tooling interfaces
- Recommended next step: tool interface review
PackagingRepeatable pick and place
Packaging tasks require stable part presentation, gripping surface review, speed expectations and recovery logic for missing or misaligned parts.
- Relevant products: grippers and automation modules
- Recommended next step: application review